“Unveiling the Ancient Art: Lost-Wax Casting Techniques for Intricate Metal Objects”
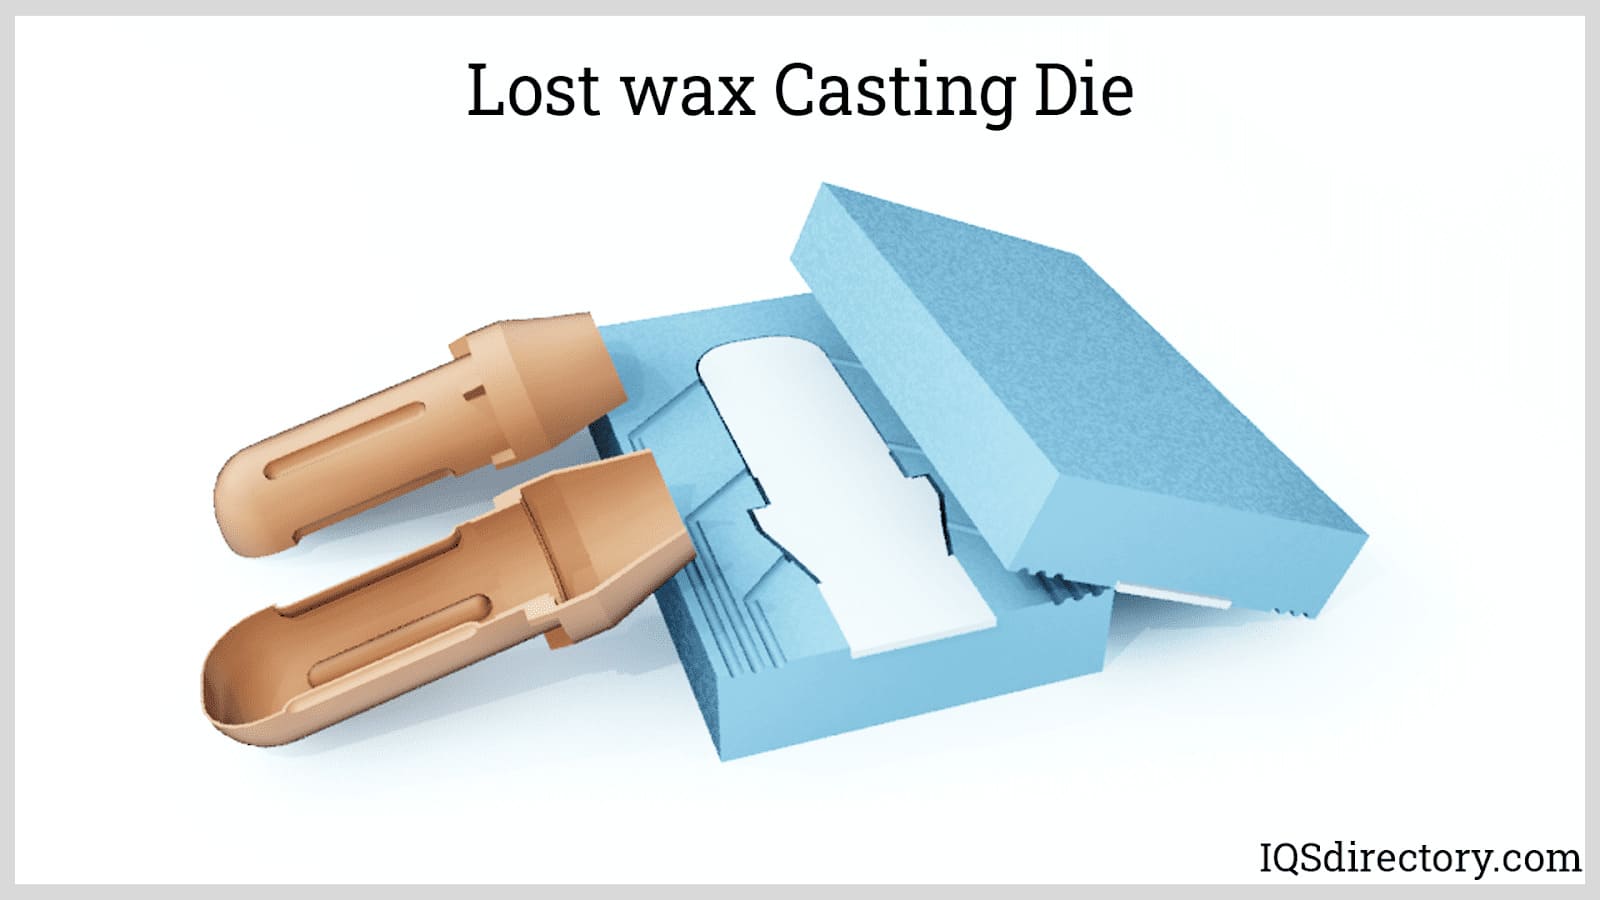
Lost-wax casting techniques have been used for centuries to create intricate and detailed metal objects. This ancient method involves creating a wax model of the desired object, encasing it in a mold, and then melting away the wax to leave a cavity that is filled with molten metal.
The first step in lost-wax casting is creating the wax model. This can be done by hand carving or by using molds made from materials such as silicone or rubber. The wax model should be an exact replica of the final product, as any imperfections will be replicated in the metal casting.
Once the wax model is complete, it is attached to a sprue, which acts as a channel through which the molten metal will flow into the mold. The sprue also helps to release any trapped air or gases during pouring.
Next, the wax model with attached sprue is dipped into a ceramic slurry or investment material. Multiple layers are applied to build up thickness and strength. After each layer dries, it may be coated with fine sand or refractory powder for additional strength and texture control.
After several layers of investment material have been applied, the entire assembly is left to dry completely before being placed in an oven or kiln for burnout. During this process, all traces of wax are melted away leaving only empty cavities within the investment material shell.
Once all of the wax has been burned out, molten metal can be poured into these cavities through small holes known as gates and vents created during mold construction. Various metals can be used for lost-wax casting including bronze, brass, silver, gold and even some non-ferrous alloys like aluminum.
As soon as pouring is complete and sufficient solidification has occurred (usually after several minutes), cooling begins so that once solidified fully; we get accurate castings without distortion due to shrinkage during cooling down period itself called Casting Lumps Control Process(CLC).
After the metal has cooled and solidified, the investment material is broken away to reveal the final metal casting. Any excess metal or rough edges can be removed through grinding, sanding, or polishing.
Lost-wax casting techniques are particularly useful for creating intricate and delicate designs that would be difficult or impossible to achieve using other methods. The process allows for fine details and smooth surfaces, making it popular in jewelry-making and sculpture.
Investment casting, also known as precision casting or lost-wax casting, is a versatile method used in blacksmithing to create complex shapes with high accuracy. It involves creating a wax model of the desired object which is then encased in a ceramic shell before being heated to remove the wax and pour molten metal into the cavity.
The first step in investment casting is to create a wax pattern of the desired object. This can be done by hand carving or by using molds made from materials such as silicone or rubber. The wax pattern should be an exact replica of the final product.
Once the wax pattern is complete, it is attached to a sprue system which includes channels for molten metal flow called runners and risers that help control porosity during solidification stage.
Next, multiple layers of ceramic slurry are applied onto the wax pattern through dipping or spraying methods. Each layer must dry completely before applying another layer until desired thickness is achieved (usually 5-10 layers).
After all layers have dried properly including drying out water content present in them; we need pre-heating process before putting them into oven where temperature goes up gradually without any sudden change otherwise possibility cracking will increase due thermal shock effect on ceramics shells created around patterns during drying operation itself called Preheating Process(PP).
Once preheating process completes successfully; actual burnout starts at relatively higher furnace temperatures ranging between 800°C – 1000°C . At this temperature range existing waxes get burnt out completely leaving behind empty ceramic shell molds.
After the burnout process, the ceramic shell molds are heated further to remove any remaining moisture and ensure their strength. Once the shells are completely dry and strong enough, they are ready for casting.
The metal is melted in a crucible or furnace at high temperature depending on type of metal being used. The molten metal is then poured into the ceramic shell mold through sprue system under controlled conditions such as vacuum or pressure to achieve desired results.
Once the metal has cooled and solidified within the ceramic shell mold, it is removed by breaking away or vibrating out the investment material. Any excess metal or rough edges can be removed through grinding, sanding, or polishing.
Investment casting allows for great precision and detail in creating complex shapes that would be difficult to achieve using other methods. It is commonly used in industries like aerospace, automotive, jewelry making etc where intricate designs need to be replicated with high accuracy without much machining work required after casting itself called Near Net Shape Casting(NNSC).
Sand casting is another widely used technique in blacksmithing that allows for intricate designs and complex shapes. It involves creating a mold made of compacted sand into which molten metal is poured. This method can produce both large-scale objects as well as small intricate parts.
The first step in sand casting is creating a pattern or replica of the desired object using materials like wood, plastic, or even metals like aluminum. This pattern will serve as a template for creating the mold.
Next, a flask (a frame-like structure) is created around the pattern by placing two halves together with sufficient space left between them known as parting line where pouring gate will come later during actual molding operation known as Molding Technique(MT).
Once the flask has been prepared; we start mixing foundry sands such silica sand along with some additives like clay,bentonite powder etc which helps holding shape better when mixed properly with water to form a sand mixture called molding sand or green sand which is then packed around the pattern in the flask.
After packing of mold, it needs to be properly vented since while pouring molten metal air should be allowed to escape during solidification stage otherwise casting will have porosity defects due trapped gases inside molds itself called Venting Process(VP).
Once mold preparation complete; we can move ahead for actual pouring operation. Molten metal is prepared in furnace or crucible at desired temperature and poured into the mold through a gating system consisting of pouring cup, sprue, runners and risers designed as per complexity involved with object being cast.
The molten metal fills the cavity created by the pattern and takes its shape. It is left to cool and solidify within the sand mold.
After solidification completes successfully; need careful handling process since hot casting can damage easily if not taken care properly. It requires removing excess sand from casting surface known as shakeout followed by cleaning operations like grinding,sanding etc depending on requirement post-casting treatments required before final usage itself called Cleaning Process(CP).
Sand casting allows for flexibility in design and is suitable for both small-scale production runs as well as single-piece creations. However, it may require additional machining work after casting to achieve desired accuracy.
Centrifugal casting methods are used when creating cylindrical objects such as pipes or tubes. This technique involves rotating a mold at high speeds while pouring molten metal into it. The centrifugal force helps distribute the molten metal evenly along the walls of the rotating mold, resulting in a uniform thickness throughout.
The first step in centrifugal casting is preparing the mold. The mold consists of two halves that fit together perfectly along their joint line. One half contains cavities or cores where inner surfaces will be formed whereas another half act like outer shell providing outer dimensions or contours respectively known as Mold Preparation (MP)
Next, these prepared molds are placed on a spinning device called a centrifuge or spinner. The mold is rotated at high speeds while molten metal is poured into it through a pouring cup or sprue system.
The centrifugal force generated by the spinning mold forces the molten metal to spread out evenly along the inner walls of the mold cavity, ensuring uniform thickness and density throughout the casting.
Once solidification completes successfully; we can remove casting from rotary device for further processing as per requirements like cooling, cleaning etc itself called Solidification Process(SP).
Centrifugal casting allows for efficient production of cylindrical objects with consistent wall thickness and minimal defects. It is commonly used in industries such as plumbing, automotive, and aerospace where pipes or tubes are required.
Vacuum casting is a method that uses negative pressure to draw molten metal into a mold. This technique ensures precise reproduction of intricate details and reduces porosity in the final product.
The first step in vacuum casting is creating a pattern or replica of the desired object using materials like wax, plastic, or even metals like aluminum. This pattern will serve as a template for creating the mold.
Next, two halves of an enclosed chamber known as flask are prepared around the pattern by placing them together properly forming closed cavity inside which pouring gate will be provided later during actual molding operation itself called Flask Preparation (FP).
Once flask preparation complete; we move ahead for preparing foundry sand mixture similar to sandcasting process but here since we require more control over quality so better grades sands along with specialized binders added which helps holding shape better when mixed properly with water known as Vacuum Casting Sand(VCS) itself called Molding Technique(MT).
After packing molds with VCS mixture; next comes venting process similar to sandcasting process mentioned earlier where air should be allowed to escape otherwise trapped gases inside molds cause porosity defects during solidification stage known as Venting Process(VP).
Once all preparations complete; actual molding operation starts where special vacuum chamber is used where molten metal is poured into the mold and negative pressure is applied to draw the molten metal into every intricate detail of the pattern.
The vacuum force helps in achieving better surface finish, improved dimensional accuracy, and reduced porosity due to trapped gases. Once solidification completes successfully; we can remove casting from mold for further processing called Solidification Process(SP).
Vacuum casting is commonly used in industries such as jewelry making, art, and prototyping where high precision and detailed reproduction are required. It allows for the production of complex shapes with minimal defects.
Continuous casting in blacksmithing is a method used to produce long lengths of metal with a consistent cross-section. This technique involves pouring molten metal into a water-cooled mold that continuously moves through various stages until it solidifies completely.
The first step in continuous casting is preparing the mold assembly. The assembly consists of a water-cooled copper or steel mold that has an open top and bottom so that molten metal can be poured into it continuously known as Mold Preparation (MP).
Next, the prepared mold assembly is positioned between two rolls or wheels that rotate at different speeds. The gap between these rolls determines the thickness of the cast product.
As the molds move through this rolling process; they gradually cool down resulting solidification process starts from outside towards inside which gives us uniform structure along entire length itself called Solidification Process(SP).
Once solidified fully; we get billet form which can be subjected next stage operation like hot rolling,cold drawing etc depending on requirement before final usage itself called Billet Processing (BP).
Continuous casting allows for efficient production of long lengths of metal with consistent dimensions throughout. It eliminates the need for multiple castings and subsequent joining processes.
Shell molding techniques are used to create unique shapes with fine details and smooth surfaces. This method involves creating a shell-like mold using resin-coated sand that provides excellent dimensional accuracy and surface finish.
The first step in shell molding is creating a pattern or replica of the desired object using materials like wood, plastic, or metal. This pattern will serve as a template for creating the shell mold.
Next, the pattern is placed in a flask and covered with a mixture of resin-coated sand. The sand is compacted around the pattern to create an even layer of uniform thickness known as Shell Mold Preparation(SMP).
Once shell mold preparation complete; we move ahead for actual pouring operation where molten metal poured into it through pouring cup,sprue system etc at designed temperature range itself called Pouring Process(PP).
After solidification completes successfully; we can remove casting from mold for further processing as per requirements like cooling,cleaning etc called Solidification Process(SP).
Shell molding techniques offer excellent dimensional accuracy and surface finish. They are commonly used in industries such as automotive, aerospace, and art where intricate designs and high-quality finishes are required.
Die casting is a widely used method in modern blacksmithing that allows for mass production of complex shapes with high precision. This technique involves injecting molten metal under high pressure into steel molds known as dies.
The first step in die casting is preparing the die assembly. The assembly consists of two halves made from heat-resistant steel that fit together perfectly along their joint line forming closed cavity inside which molten metal will be injected itself called Die Assembly (DA).
Next, the prepared die assembly is mounted onto a machine known as a die-casting machine or press. Molten metal is melted in furnace or crucible at desired temperature and injected into the die cavity under high pressure through sprue system consisting gate runners risers etc itself called Injection Process(IP).
As soon injection process starts; rapid cooling takes place since dies being made up heat resistant material so they also absorb some heat but due to coolant passages provided through them helps pulling away heat faster resulting solidification happens within seconds only thus leading good dimensional accuracy, surface finish etc itself called Solidification Process(SP).
Once solidification completes successfully; we can open the die halves and remove casting from mold for further processing as per requirements like cooling,cleaning etc called Mold Opening & Extraction(MOE).
Die casting allows for high production rates and is commonly used in industries such as automotive, electronics, and consumer goods where mass production of complex shapes with tight tolerances is required.
Spin casting, also known as centrifugal rubber mold casting, is a method used to produce small-scale production runs of metal objects. This technique involves creating a reusable rubber mold that is spun at high speeds while molten metal is poured into it.
The first step in spin casting is creating a master pattern or replica of the desired object using materials like wax or plastic. This pattern will serve as a template for creating the rubber mold.
Next, the master pattern is embedded in a special silicone-based material that hardens to form a flexible rubber mold around it. The mold should have an opening through which molten metal can be poured later known as Rubber Mold Preparation (RMP).
Once rubber mold preparation completes successfully; next comes actual spinning process where this prepared molds are placed on spinning device similar to centrifuge but here since we require more control so speed rotation controlled better resulting precise castings without much defects due uneven filling during pouring operation itself called Spinning Process(SP).
As soon spinning starts; molten metal poured into it through pouring cup,sprue system etc at designed temperature range under controlled conditions such pressure,vacuum etc itself called Pouring Process(PP).
After pouring process completes successfully; we can stop spinning process allowing filled molds cool down naturally within few minutes only thus leading good dimensional accuracy without much mechanical work required aftercasting itself called Solidification Process(SP).
Once solidified fully; we get accurate castings without distortion due to shrinkage during cooling down period thus leading reduced machining cost aftercasting itself called Solidification Process(SP).
Spin casting is commonly used in industries such as jewelry making, model making, and prototyping where small-scale production runs of detailed metal objects are required.
Ceramic shell casting is a technique used to produce high-quality metal objects with fine details and smooth surfaces. This method involves creating a ceramic mold that can withstand the high temperatures of molten metal.
The first step in ceramic shell casting is creating a pattern or replica of the desired object using materials like wax or plastic. This pattern will serve as a template for creating the ceramic mold.
Next, multiple layers of ceramic slurry are applied onto the pattern through dipping or spraying methods. Each layer must dry completely before applying another layer until desired thickness is achieved itself known as Ceramic Mold Preparation (CMP).
Once ceramic mold preparation complete successfully; next comes actual pouring operation where molten metal poured into it through pouring cup,sprue system etc at designed temperature range under controlled conditions such pressure,vacuum etc itself called Pouring Process(PP).
After solidification completes successfully; we can remove casting from mold for further processing as per requirements like cooling,cleaning etc called Solidification Process(SP).
Ceramic shell casting allows for excellent dimensional accuracy and surface finish due to its ability to reproduce fine details. It is commonly used in industries such as aerospace, art, and jewelry making where high-quality finishes are required.
Cold chamber die casting is a variation of die casting that allows for the production of larger and heavier parts. This technique involves melting the metal in an external furnace before transferring it to a separate cold chamber where it is injected into the dies under high pressure.
The first step in cold chamber die casting is preparing the dies assembly similar to conventional diecasting process mentioned earlier but here since we require more control over temperature so better grades steel molds along with coolant passages provided through them helps pulling away heat faster resulting accurate castings without much defects due thermal shock effect on dies itself called Die Assembly (DA).
Next, the prepared die assembly is mounted onto a machine known as a cold chamber die-casting machine or press. The molten metal is melted in an external furnace at desired temperature and transferred to the cold chamber where it is injected into the dies under high pressure through sprue system consisting gate runners risers etc itself called Injection Process(IP).
As soon injection process starts; rapid cooling takes place since dies being made up heat resistant material so they also absorb some heat but due to coolant passages provided through them helps pulling away heat faster resulting solidification happens within seconds only thus leading good dimensional accuracy, surface finish etc itself called Solidification Process(SP).
Once solidification completes successfully; we can open the die halves and remove casting from mold for further processing as per requirements like cooling,cleaning etc called Mold Opening & Extraction(MOE).
Cold chamber die casting allows for the production of larger and heavier parts with high precision. It is commonly used in industries such as automotive, aerospace, and machinery manufacturing.
Low-pressure permanent mold casting methods are used to produce complex-shaped metal objects with consistent quality. This technique involves filling a reusable metallic mold with molten metal using low pressure rather than high pressure.
The first step in low-pressure permanent mold casting is preparing the reusable metallic mold assembly similar to sandcasting process mentioned earlier but here since we require more control over molds so better grades metals along with specialized coatings applied which helps holding shape better when subjected mechanical forces during pouring operation known as Mold Preparation (MP).