Mastering the Art of Forge Welding: Techniques, Flux Selection, and Troubleshooting
Flux selection for forge welding:
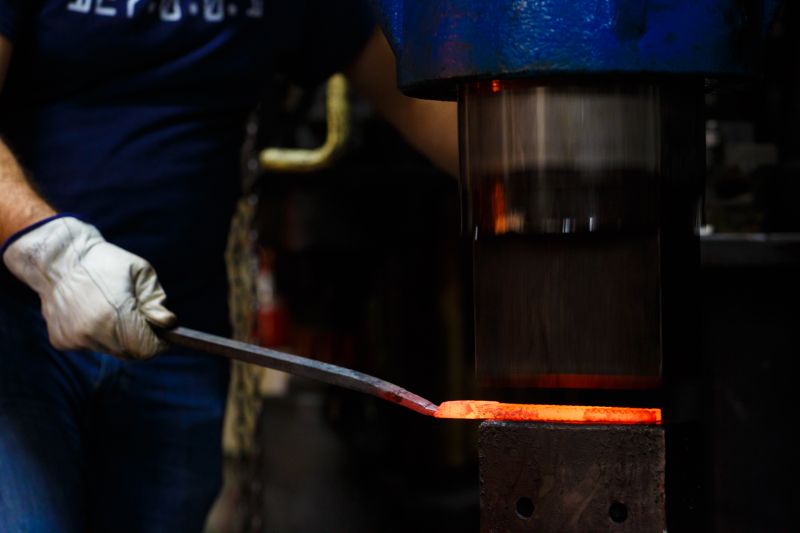
Forge welding is a crucial technique in blacksmithing and metalworking that allows two or more pieces of metal to be joined together permanently. One key element in achieving successful forge welds is the use of flux. Flux serves multiple purposes during the welding process, including preventing oxidation, removing impurities, and facilitating the flow of molten metal.
When selecting a flux for forge welding, it’s important to consider several factors such as the type of metals being welded, the temperatures involved, and personal preference. There are various types of fluxes available on the market, each with its specific properties and applications.
Borax is one of the most commonly used fluxes in forge welding. It has excellent deoxidizing properties and helps remove scale from heated metals. Borax forms a glassy layer on the surface of the metal when heated, which acts as a barrier against oxygen and prevents further oxidation during forging. Borax is readily available and relatively inexpensive, making it a popular choice among blacksmiths.
Another frequently used flux is powdered iron oxide (commonly known as red iron oxide or red rouge). Iron oxide works effectively at high temperatures and can withstand prolonged heating without breaking down. It creates a protective layer on steel surfaces while enabling clean welds.
Silica sand mixed with borax can also serve as an effective flux for forge welding stainless steel. The combination provides both deoxidizing properties from borax and silica’s ability to form slag that shields against oxidation during heating.
For copper and brass alloys, phosphate-based fluxes are often preferred due to their ability to dissolve oxides effectively at lower temperatures compared to borax-based alternatives. These low-temperature phosphates prevent excessive scaling while promoting good adhesion between the metals being welded.
When working with aluminum alloys, specialized aluminum-specific fluxes are necessary due to their unique characteristics. Aluminum requires higher temperatures than other metals for proper forge welding, and fluxes designed for aluminum help remove the oxide layer and promote bonding.
Forge welding titanium can be challenging due to its high reactivity with oxygen at elevated temperatures. To successfully forge weld titanium, a combination of argon gas shielding and specialized titanium-specific flux is often used. The flux aids in removing oxides while the inert atmosphere provided by argon prevents further oxidation during the welding process.
High carbon steels require specific fluxes that can handle the high temperatures involved. Fluxes containing barium carbonate or calcium fluoride are commonly used as they have excellent deoxidizing properties and reduce scaling on the steel’s surface.
Welding dissimilar metals in the forge requires careful selection of flux to ensure proper bonding between different materials. In such cases, using a highly active flux like borax is recommended to aid in removing oxide layers from both metals being welded.
Troubleshooting common issues in forge welding:
Despite following proper techniques and using suitable fluxes, issues may still arise during forge welding. Some common problems encountered include incomplete fusion, lack of penetration, porosity, cracks, or weak welds.
Incomplete fusion occurs when there is insufficient heat or pressure applied during the welding process. It can be resolved by reheating the joint until it reaches an appropriate temperature for complete fusion to occur.
Lack of penetration happens when molten metal fails to penetrate fully into the joint being welded. This issue can be addressed by adjusting heat levels or applying more pressure during forging.
Porosity refers to small holes or voids within a weld caused by trapped gases or impurities. Using cleaner metal surfaces before forging and selecting appropriate fluxes that help eliminate impurities can minimize porosity issues.
Cracks in forged welds may result from improper heating or cooling processes. Ensuring even heating throughout the workpiece followed by controlled cooling through annealing can help prevent cracking.
Weak welds occur when there isn’t sufficient metallurgical bonding between two pieces of metal. This issue can be resolved by ensuring proper flux application, sufficient heat, and adequate pressure during the welding process.
It’s important to note that troubleshooting forge welding issues requires practice, experience, and a good understanding of the metallurgical properties of the metals being welded. Regularly reviewing and analyzing failed welds can help identify areas for improvement in technique or flux selection.
Preparing surfaces for successful forge welds:
Proper surface preparation is crucial for achieving successful forge welds. The metal surfaces being joined must be clean and free from oxides, scale, dirt, and other contaminants that could hinder the bonding process.
Before forge welding, it is essential to remove any rust or mill scale from the metal surfaces. This can be done using wire brushes or abrasive cleaning methods such as sanding or grinding. Care should be taken to avoid overheating the metal during this process.
After cleaning the surfaces, applying an appropriate flux helps prevent oxidation during heating and facilitates better adhesion between the metals. The flux should be evenly distributed over both mating surfaces before they are brought together.
Once the workpiece is assembled with proper alignment, it is heated to a suitable temperature based on the type of metal being welded. Uniform heating throughout the joint area ensures consistent bonding between the metals.
Welding techniques for complex geometries:
Forge welding complex geometries requires careful planning and execution to ensure proper fusion between different parts of a workpiece. Some common techniques used in these situations include scarf welding, lap joints, butt joints with inserts or wedges-called “jump” welds-and dovetail joints.
Scarf welding involves tapering one end of each piece being joined to create an overlapping joint surface when brought together under heat and pressure. This technique provides increased contact area for better fusion between components with irregular shapes or angles.
Lap joints involve overlapping two pieces partially along their length before forging them together. This method works well when joining flat or thin pieces that can be easily overlapped.
Butt joints with inserts or wedges, known as “jump” welds, are useful when joining thick or heavy sections. An insert or wedge is inserted between the two mating surfaces to provide additional material for bonding and increase joint strength.
Dovetail joints involve creating interlocking grooves and ridges in the two pieces being joined. The dovetail shape increases contact area and provides mechanical support during heating and forging.
Each welding technique has its advantages and limitations depending on the complexity of the geometry involved. It’s important to choose the appropriate method based on the design requirements of the finished piece.
Joining techniques for decorative elements in forged pieces:
In forge welding, not only functional components but also decorative elements can be added to enhance a finished piece’s aesthetics. Joining these decorative elements requires specific techniques to ensure they are securely attached without compromising their visual appeal.
One commonly used method is plug welding, which involves drilling small holes into one metal surface before bringing it into contact with another surface under heat and pressure. This technique allows for precise placement of decorative elements while ensuring good fusion between metals.
Another technique is stitch welding, where multiple smaller welds are made along a seam or patterned area. This creates an attractive visual effect while providing structural integrity to delicate designs.
For more intricate work, soldering or brazing can be used instead of traditional forge welding methods. These techniques involve using lower temperatures and filler materials like silver solder or brass rod to join different metal parts together without compromising their appearance.
The choice of joining technique depends on factors such as design requirements, materials being used, and personal preference in achieving desired aesthetic results while maintaining durability.
The art of forge brazing as an alternative to traditional welding methods:
Forge brazing is a specialized form of metal joining that uses heat combined with filler material (brazing alloy) applied at temperatures below melting points of base metals. This process allows for the joining of dissimilar metals or delicate components that might be damaged by traditional forge welding techniques.
In forge brazing, flux is used to prevent oxidation and promote wetting of the base metals by the filler material. The workpiece is heated until the brazing alloy melts and flows into the joint, creating a strong bond between different parts.
One advantage of forge brazing is its ability to join metals with significantly different melting points. It also requires less heat compared to traditional forge welding, reducing the risk of distortion or damage to delicate pieces.
Forge brazing can be an excellent choice when working with non-ferrous metals like copper, brass, or bronze alloys that have low melting points compared to steel or iron. It enables intricate designs and decorative elements to be incorporated into metalwork without compromising their integrity.
Exploring historical forge welding techniques and their applications today:
While modern blacksmiths have access to advanced equipment and materials, it’s valuable to explore historical forge welding techniques that were used in ancient times. These techniques not only provide insight into how early civilizations forged metal but can also offer alternative methods for contemporary blacksmiths.
One such technique is fire welding, which involves heating two separate pieces of metal in a forge until they reach a malleable state before quickly bringing them together under pressure. Fire welding relies on precise timing and coordination between heating both pieces simultaneously while ensuring they remain hot during forging.
Another historical technique is scarfed lap joints where one end of each piece being joined is tapered before being overlapped under heat and pressure. Scarf joints were commonly used in shipbuilding during ancient times due to their strength and reliability.
Pattern-welded steel (commonly known as damascus steel) was another historically significant technique involving layering different types of iron or steel together before forging them under intense heat. This process created visually striking patterns while producing blades with exceptional strength and sharpness.
By exploring and studying these historical forge welding techniques, modern blacksmiths can gain a deeper understanding of the craft while incorporating elements of tradition into their own work.