Mastering the Art of Brazing: Unlocking Strong and Reliable Joints
Brazing is a widely used joining technique in the manufacturing industry, offering several advantages over other methods such as welding or soldering. It involves melting a filler metal and using it to join two or more base metals together. However, successful brazing requires careful consideration of various factors, from selecting the right flux to understanding the impact of temperature and joint design on the strength of the braze.
One critical aspect in brazing is flux selection. Fluxes are materials that are applied to the joint area before brazing to prevent oxidation and promote wetting between the filler metal and base metals. The choice of flux depends on factors such as material compatibility, application temperature, and post-braze cleaning requirements. Common types of flux include boron-based fluxes for copper alloys, aluminum-based fluxes for aluminum alloys, and chloride-based fluxes for stainless steels.
Troubleshooting joint failures in brazing can be challenging but crucial for ensuring strong and reliable joints. Joint failures can occur due to issues like insufficient heating or cooling rates, inadequate surface preparation, incorrect filler metal selection, or poor joint design. By carefully analyzing failed joints through techniques like visual inspection and microstructural analysis, it becomes possible to identify the root causes of failure and implement corrective measures.
Brazing stainless steel alloys presents unique challenges compared to other materials due to their high thermal conductivity and chromium oxide layer that forms on their surfaces. To overcome these challenges, it is essential to select specialized filler metals with good corrosion resistance properties along with appropriate fluxes designed specifically for stainless steels.
Advanced techniques such as torch brazing offer increased control over heat input during the process. This method uses a flame torch combined with a filler rod or pre-placed alloy foil to join components together effectively. Torch brazing is commonly used in applications where precise control over localized heating is required.
Temperature plays a crucial role in brazing as it determines not only how well the filler metal flows but also the metallurgical properties of the joint. Understanding the relationship between temperature, filler metal, and base metals is vital to achieve strong and durable brazed joints. Factors like preheating, heating rates, soaking time, and cooling rates need to be carefully controlled to minimize thermal stresses and ensure successful brazing.
High-temperature brazing requires the selection of appropriate filler metals that can withstand elevated temperatures without losing their strength or other desirable properties. Nickel-based alloys, silver-based alloys, and gold-based alloys are commonly used for high-temperature applications due to their excellent mechanical strength at elevated temperatures.
Brazing dissimilar metals can be challenging due to differences in thermal expansion coefficients and melting points. However, there are several solutions available such as using a transition material or employing active brazing techniques that promote intermetallic bonding between dissimilar materials.
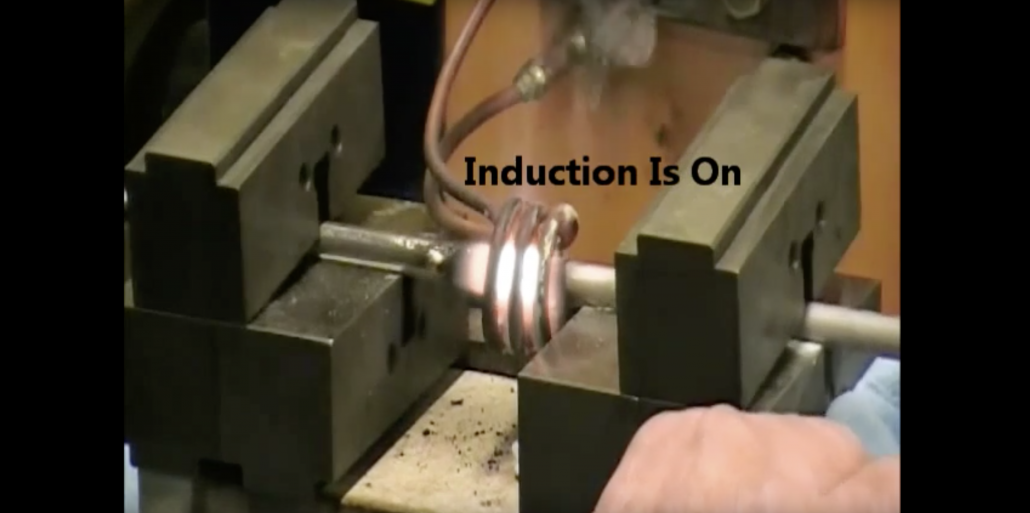
While torch brazing is a popular method, alternative methods like induction brazing offer advantages in terms of energy efficiency and localized heating. Induction brazing uses electromagnetic fields to generate heat within the workpiece directly rather than relying on external heat sources.
Proper surface preparation is crucial for achieving strong braze joints. Surfaces should be clean and free from contaminants such as oils, oxides, or scale before applying fluxes or filler metals. Techniques like cleaning with solvents or mechanical abrasion can help ensure optimal surface conditions for successful brazing.
Vacuum brazing offers several advantages such as reduced oxidation and improved cleanliness compared to traditional atmospheric brazing methods. However, it comes with limitations in terms of equipment complexity and cost-effectiveness for large-scale production.
Brazing copper alloys requires specialized techniques due to their high thermal conductivity. Preheating the components helps reduce thermal gradients during heating while ensuring proper wetting by controlling oxide formation on the surface before applying fluxes or filler metals.
Fluxless brazing techniques have gained attention in specific applications where avoiding residual flux is critical. These techniques rely on the use of specialized filler metals or coatings that eliminate the need for fluxes, reducing post-braze cleaning requirements.
Preheating considerations in induction brazing involve determining the optimal preheat temperature to ensure proper wetting and flow of filler metal while minimizing thermal gradients and stresses during brazing.
Active metal brazes can be used to join ceramics, which are typically difficult to bond due to their high melting points and chemical inertness. Active metal brazes contain reactive elements that form compounds with ceramic surfaces, enabling strong joints between ceramics and other materials.
After brazing, flux residues must be removed from the joint area to prevent corrosion or reduce surface contamination. Flux removal methods include mechanical brushing, washing with solvents or hot water, or using ultrasonic cleaning techniques depending on the specific application requirements.
The design of a braze joint significantly influences its strength and reliability. Factors such as joint clearance, fillet size, base metal thickness, and geometrical configuration all play a role in determining the final strength of the joint.
Selective area heating in laser-assisted brazing offers precise control over heat input by using lasers to selectively heat specific areas during the process. This technique is particularly useful when joining components with localized heat-sensitive areas or complex geometries.
Microstructural analysis is essential for evaluating braze joints’ quality and understanding their mechanical properties. Techniques like optical microscopy, scanning electron microscopy (SEM), energy-dispersive X-ray spectroscopy (EDS), or X-ray diffraction (XRD) can provide valuable insights into grain structure, intermetallic formation, elemental distribution, and phase identification within the joint region.
Brazing aluminum alloys presents challenges due to their oxide layer formation at elevated temperatures. However, specialized fluxes designed for aluminum alloys along with appropriate filler metals can facilitate successful brazing while maintaining good joint strength.
Residual stresses can develop within a braze joint during cooling, which can affect its mechanical properties and long-term reliability. Understanding the effects of residual stresses and implementing strategies to minimize them, such as controlled cooling or stress-relief heat treatments, is crucial for ensuring robust brazed joints.
In conclusion, brazing offers a versatile joining technique with numerous applications across various industries. By carefully considering factors like flux selection, temperature control, joint design, and surface preparation, it is possible to achieve strong and reliable braze joints in a wide range of materials and applications. Additionally, exploring advanced techniques, alternative methods, and understanding microstructural aspects can further enhance brazing processes’ efficiency and effectiveness.