Forging Ahead: Unveiling the Contrasts Between Open Die and Closed Die Forging
Differences between Open Die and Closed Die Forging
When it comes to blacksmithing, one of the most important processes is forging. Forge work involves shaping metal by applying pressure through various techniques. Two common methods used in forging are open die and closed die forging. Both approaches have their own advantages and applications, making them essential knowledge for any modern blacksmith.
In this article, we will delve into the differences between open die and closed die forging, exploring their unique characteristics, pros and cons, as well as the specific scenarios where each method is best suited.
1. Definition:
Open Die Forging:
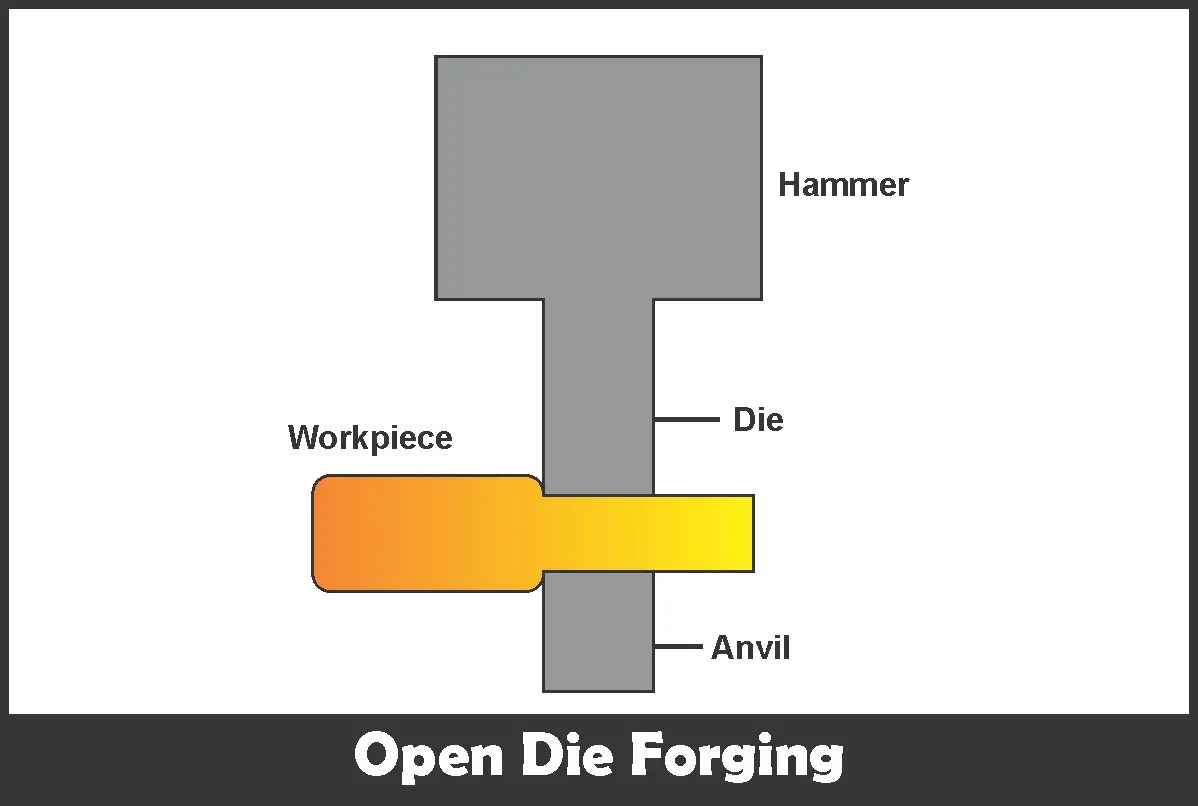
Open die forging, also known as smith hammer or flat-die forging, is a technique that involves manipulating metal between two flat dies without completely enclosing it. The dies are usually large in size with no impression cavities or shapes preformed on them.
Closed Die Forging:
Closed die forging, often referred to as impression-die or drop-forging, entails shaping metal within custom-designed molds called dies. The dies have impressions matching the desired final shape of the forged piece.
2. Process:
Open Die Forging:
The open die process begins with heating a piece of metal until it reaches an optimal temperature for shaping (above its recrystallization temperature). Once heated properly using a forge furnace or other heat sources like induction heating systems or gas furnaces, the hot metal is placed onto an anvil-like surface between two large flat-faced hammers called tup dies.
The blacksmith then strikes the top hammer forcefully onto the hot metal while controlling its movement using precise hand-eye coordination skills. This repeated striking causes plastic deformation in the workpiece which gradually takes on the desired shape under controlled blows.
Closed Die Forging:
In closed die forging, accurately machined upper and lower dies are employed to enclose and shape heated material according to predefined designs within a press machine’s frame. The raw material is first heated to a suitable temperature, allowing for better plasticity and reducing the risk of cracking during deformation.
Once heated, the metal is placed within the closed die cavity, and force is applied through a hydraulically or mechanically operated press. The pressure exerted on the material causes it to flow into the impressions created by the dies, resulting in precise shaping of the final product.
3. Material Shapes:
Open Die Forging:
Due to its nature of using flat-faced dies without any specific shape impressions, open die forging offers tremendous versatility in terms of size and shape possibilities. This method is ideal for producing large forgings such as shafts, discs, cylinders, blocks, and other simple geometries with minimal complexity.
Closed Die Forging:
The closed die process allows for intricate designs and complex shapes. By utilizing custom-designed dies with carefully crafted impressions matching desired end products’ specifications, closed die forging can produce parts with high precision and intricate details. It is well-suited for manufacturing components like gears, crankshafts, connecting rods, valves bodies etc., that require tight tolerances or unique features.
4. Equipment Requirements:
Open Die Forging:
Since open die forging relies more on manual skill and craftsmanship rather than specialized equipment or machinery alone; it requires relatively less investment in terms of infrastructure. The primary tools needed are an anvil-like surface (such as a blacksmith’s table) along with heavy-duty hammers suitable for striking hot metal repeatedly.
Closed Die Forging:
Compared to open-die forging methods where hammers play a crucial role in shaping metal manually; closed-die forging necessitates more sophisticated machinery like hydraulic presses or mechanical presses capable of generating high pressure forces required to close the dies around hot metal pieces firmly.
5. Production Volume:
Open Die Forging:
Open die forging often caters to low-volume production due to its manual nature requiring skilled labor intervention throughout each stage of forming processes. However, with experienced blacksmiths and efficient work practices, the production rate can still be satisfactory for small to medium-sized batches of forgings.
Closed Die Forging:
Closed die forging is well-suited for high-volume production due to its ability to produce multiple parts simultaneously using automated press machines. The closed cavity design ensures consistent piece-to-piece quality while maintaining tight dimensional control. This method significantly reduces overall manufacturing time and allows for economies of scale.
6. Material Usage Efficiency:
Open Die Forging:
As open die forging relies on skillful manual hammering techniques, it may result in a less efficient material usage compared to closed die forging. The repeated blows during shaping can lead to some material wastage as excess metal is removed or trimmed away in order to achieve the desired final shape.
Closed Die Forging:
In contrast, closed die forging offers superior material usage efficiency since it limits waste through precise impressions that closely match the final product’s dimensions. With minimal trimming or machining required after forging, this method optimizes material utilization and minimizes scrap generation.
7. Surface Finish:
Open Die Forging:
Due to the nature of open-die forging where contact occurs between hot metal and flat-faced dies, components produced by this method typically exhibit a rougher surface finish requiring additional machining operations like grinding or milling if a smoother finish is desired.
Closed Die Forging:
The use of carefully designed impressions in closed-die forging leads to improved surface finishes directly from the mold itself. While some minor post-forging finishing might still be required depending upon specific requirements; overall, products forged using this approach tend to have better surface finishes than those produced via open-die methods.
8. Cost Considerations:
Open Die Forging:
The cost associated with open-die forgings tends to be lower compared to closed-die forgings since it requires less specialized equipment and infrastructure investment upfront. Additionally, smaller batch sizes make it more suitable for low-volume or custom manufacturing.
Closed Die Forging:
Closed die forging often involves higher upfront costs due to the need for specialized machinery, dies, and tooling. However, as production volumes increase, economies of scale start to play a significant role in reducing per-unit costs. The ability to produce multiple parts at once also increases efficiency and lowers manufacturing expenses over time.
Conclusion:
Both open die and closed die forgings are valuable techniques used by modern blacksmiths to shape metal into desired forms. Open die forging provides versatility in terms of size and simplicity of shapes while closed die forging excels at producing complex designs with high precision.
The choice between these methods depends on various factors including desired product characteristics, volume requirements, cost considerations, and surface finish expectations. Understanding the differences between open die and closed-die forging allows blacksmiths to select the most appropriate method for each specific project, leading to efficient production processes and exceptional end products that meet customer needs.