“Unveiling the Ancient Art of Lost-Wax Casting: Intricate Metal Pieces Crafted with Skill and Detail”
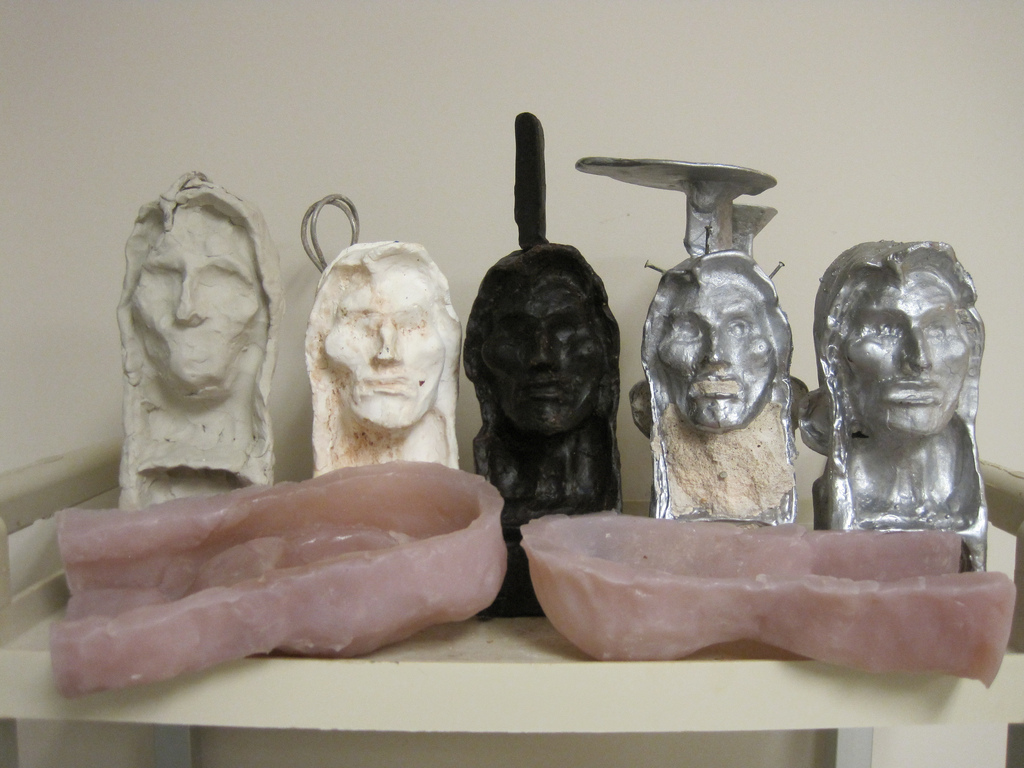
Lost-wax casting techniques have been used for centuries in blacksmithing to create intricate and detailed metal pieces. This method involves creating a wax model of the desired shape, encasing it in a ceramic mold, and then melting away the wax to leave a hollow space that is filled with molten metal.
The process begins with sculpting or carving the wax model by hand or using specialized tools. The wax should be melted and poured into a pre-made mold or carved directly into the desired shape. Once the wax model is complete, it is attached to a pouring cup, which will serve as the entry point for molten metal.
Next, several layers of ceramic material are applied over the wax model to form a mold. These layers may consist of plaster, silica sand, or other refractory materials mixed with water. Each layer needs time to dry before applying another layer. After all layers are applied and dried completely, the entire assembly is heated in an oven or furnace to melt away the wax (hence “lost-wax”).
Once all traces of wax have been removed from the mold, it is ready for casting. Molten metal – often bronze or brass – is poured into the cavity through the pouring cup. The mold must be handled carefully at this stage to prevent cracking or breakage due to thermal shock caused by contact with hot metal.
After allowing sufficient time for cooling and solidification (which can vary depending on factors like size and type of metal), the mold is broken open revealing a rough cast piece that closely resembles the original wax model but made out of metal instead.
The rough cast piece then undergoes further finishing processes such as grinding, polishing, filing, and sometimes soldering if multiple parts need joining together.
While lost-wax casting allows for great detail and complexity in blacksmithing projects, it can be time-consuming and requires skillful craftsmanship. However,, its versatility makes it suitable for various applications including jewelry making, sculpture, and decorative pieces.
Sand casting is another popular technique used by blacksmiths for creating metal objects. It involves making a mold out of sand by packing it tightly around a pattern or model. This method is particularly useful for larger projects or when intricate details are not necessary.
To start the process, a wooden or metal pattern is made in the shape of the desired object. The pattern can be carved by hand or fabricated from other materials such as clay or plastic. The pattern is then pressed into prepared sand to create an impression.
The sand must have certain qualities to ensure successful casting – it should be able to withstand high temperatures without collapsing, have good permeability to allow gases and steam escape during casting, and be easily compacted around the pattern.
Once the sand mold is prepared, molten metal is poured into the cavity through a gating system that allows for proper flow and filling of the mold. After cooling and solidification, the sand mold is broken apart revealing the casted piece.
Unlike lost-wax casting, sand casting does not provide as much detail but makes up for it with its simplicity and cost-effectiveness. It also allows for flexibility in terms of material choice as various metals like iron, steel, aluminum can be cast using this method.
Investment casting (also known as precision casting) has gained popularity in modern blacksmithing due to its ability to produce highly accurate and detailed parts with smooth surface finishes. This process starts with creating a wax model that matches the final product’s dimensions precisely.
The wax model is then coated with several layers of ceramic material until it forms a hard shell around it. Once dry, this ceramic shell assembly undergoes heating in order to melt away any remaining wax inside (similarly to lost-wax casting).
Afterward,, molten metal – usually non-ferrous alloys like bronze or brass – is poured into the hollow space left behind after removing wax. The metal fills the mold completely, taking the shape of the wax model.
Once cooled and solidified, the ceramic shell is broken away to reveal the casted piece. Investment casting allows for intricate details and thin sections in castings that would be difficult to achieve with other methods.
Centrifugal casting involves spinning a mold filled with molten metal at high speeds to distribute it evenly within the mold cavity. This method produces dense and defect-free castings by utilizing centrifugal force to overcome gravity during solidification.
To start, a hollow cylindrical or conical-shaped mold is prepared. Molten metal – often iron or steel – is poured into the center of the rotating mold while centrifugal force spreads it uniformly across the inner surface.
As cooling takes place, impurities are forced towards the center due to their lower density compared to molten metal. This allows for cleaner and more homogeneous castings without porosity or voids.
Centrifugal casting is commonly used for producing pipes, tubes, cylinders, and wheel rims where high-quality materials are required.
Vacuum casting is a technique used when working with highly detailed or delicate designs that require precise reproduction. It involves using a vacuum chamber to remove air from both the mold cavity and molten metal before pouring it into the mold.
To begin this process, a two-piece silicone rubber mold is created from an original pattern or model. The molds are then assembled together tightly around sprue channels through which molten metal will flow into each individual cavity within them when poured later on.
Next,, these assembled molds are placed inside a vacuum chamber where air pressure inside it gets reduced significantly (usually below atmospheric level) by removing any trapped gases present within both cavities as well as liquid metals being used too before finally sealing off access points leading outwards entirely so nothing else can enter after evacuation occurs successfully!
The vacuum chamber has various applications in blacksmithing such as creating intricate jewelry pieces, small-scale sculptures, or prototypes for larger projects. It ensures that the castings are free from defects like air bubbles and porosity by eliminating trapped air before casting.
Spin casting, also known as centrifugal rubber mold casting or high-pressure diecasting, is a technique used to produce small-to-medium-sized objects with excellent detail and surface finish. This method utilizes a reusable rubber mold that is spun at high speeds while molten metal is poured into it.
To begin this process, a master pattern – typically made of wax or plastic – is created in the desired shape. The pattern is then attached to a central sprue base which will serve as the entry point for molten metal.
The rubber mold material – usually silicone-based – is poured around the pattern and allowed to cure. Once cured, the mold is cut open along predetermined lines to allow easy removal of both pattern and sprue base.
Next,, the assembled mold is placed onto a spin caster machine where it can be rotated at high speeds. Molten metal – often zinc or pewter alloys due to their low melting points – is heated until liquefied before being poured into the spinning mold through its central sprue hole.
Centrifugal force caused by rotation spreads the molten metal evenly throughout each cavity within the mold, ensuring complete filling and capturing all details present on patterns’ surfaces without any visible defects like voids or porosity when solidified later on!
After giving sufficient time for cooling and solidification (usually achieved through water-cooling after pouring), molds are removed from machines carefully reveal castings with accurate dimensions matching original patterns perfectly!
Spin casting offers several advantages over other methods such as faster production times due to shorter cooling periods between pours since they’re smaller volumes involved overall plus easier replication complex shapes because of flexibility afforded by using soft materials making them ideal choices certain applications such jewelry-making prototyping!.
Die casting is an industrial manufacturing process used for producing large quantities of metal components with high precision and consistent quality. It involves injecting molten metal into a mold cavity under high pressure.
To start the process, a two-part steel mold is created that matches the final shape of the desired component. The mold consists of two halves – a fixed half called the “cover die” and a movable half known as the “ejector die.” These halves are precisely machined to create cavities for forming the part.
The molten metal, typically aluminum or zinc alloys, is injected into the mold at high speeds using hydraulic or mechanical forces. The metal fills up all cavities within the mold, taking on its shape.
Once cooled and solidified, the mold halves are separated, and the finished part is ejected from the ejector die using pins or air blasts. Any excess material in gate areas (where molten metal enters) is trimmed off before moving to further finishing processes like deburring or machining if required.
Die casting offers several advantages over other casting methods such as excellent dimensional accuracy, smooth surface finishes, and fast production rates due to its ability to produce complex shapes in large volumes repeatedly. This makes it suitable for industries requiring mass production of components like automotive or consumer electronics manufacturing.
Continuous casting is a method used primarily in steelmaking but can also be applied to non-ferrous metals like copper or aluminum. It allows for continuous production of billets (semi-finished products) without interruption by pouring molten metal into water-cooled molds that are continuously withdrawn from themold assembly line.
The process starts with melting raw materials in an electric arc furnace or basic oxygen furnace until they reach their liquid state at temperatures above their melting points. The liquid metal then flows through a tundish (a reservoir) where it’s held temporarily before being poured into multiple molds simultaneously through small openings called nozzles.
As each strand of solidifying cast passes through various cooling zones within water-cooled molds, it gradually solidifies into a continuous billet or slab with uniform cross-section. The cast product is then cut to desired lengths using torches or blades before moving on to further processing like rolling, forging, or extrusion.
Continuous casting offers several advantages over traditional ingot casting methods such as better quality control due to reduced segregation and improved microstructure in the final product. It also eliminates the need for subsequent reheating processes since the material remains hot after casting.
Shell molding (also known as shell mold casting) is a precision metal casting process that produces accurate and smooth-surface finish parts by utilizing resin-coated sand molds. This method combines features of both sand casting and investment casting.
To begin this process, a pattern made of wood, plastic, or metal is created in the shape of the desired part. The pattern is then coated with a thin layer of thermosetting resin and covered with fine silica sand mixed with a catalyst-like phenolic urethane resin.
The coated pattern is placed inside an oven where the heat cures the resin mixture forming a hard shell around it. Once cured, excess sand is removed from around the shell leaving behind an empty cavity that matches original patterns’ dimensions precisely!
Afterward,, two halves are joined together tightly along predetermined parting lines creating complete mold assembly ready for pouring molten metal into it through gates designed specifically allowing proper flow filling without any turbulence occurs during this stage!
Once cooled down enough time given solidify completely before breaking open revealing finished casts accurate details surface finishes possible!