Mastering the Art of Welding: Techniques, Advantages, and Limitations
Flux-cored arc welding (FCAW):
Flux-cored arc welding (FCAW) is a popular welding process that combines the benefits of both shielded metal arc welding (SMAW) and gas metal arc welding (GMAW). FCAW uses a continuous tubular electrode filled with flux that provides a shielding gas to protect the weld pool from atmospheric contamination. This makes FCAW suitable for outdoor applications where wind can blow away the shielding gas in other processes.
One of the main advantages of FCAW is its high deposition rate, which allows for faster welding compared to other processes. The flux in the electrode also improves the quality of the weld by providing better control over impurities and reducing porosity. Additionally, FCAW is versatile and can be used on a variety of materials including carbon steel, stainless steel, and even some non-ferrous metals.
However, like any welding process, FCAW has its limitations. It produces more smoke and fumes compared to other processes due to the flux core. Therefore, proper ventilation or respiratory protection is crucial when performing FCAW. Also, because it relies on an external shielding gas provided by the flux core, it may not be suitable for certain applications where precise control over shielding gases is required.
Electron beam welding (EBW):
Electron beam welding (EBW) is an advanced fusion-welding process that utilizes a highly focused beam of electrons to join metals together. In EBW, electrons are accelerated to high speeds using electromagnetic fields before being concentrated into a narrow beam directed at the workpiece.
One key advantage of EBW is its ability to produce deep penetration welds with minimal distortion or heat-affected zones. This makes it ideal for joining thick materials or dissimilar metals without compromising their mechanical properties. Furthermore, EBW offers excellent control over heat input since most of it goes directly into melting the metal, resulting in precise and high-quality welds.
However, EBW also has some drawbacks. The process requires a vacuum environment to prevent the electrons from scattering, which can be expensive and time-consuming to set up. Additionally, the equipment for EBW is costly and complex, making it less accessible for small-scale operations or hobbyists. Despite these limitations, EBW finds applications in industries such as aerospace, automotive manufacturing, and medical device fabrication.
Friction stir welding (FSW):
Friction stir welding (FSW) is a solid-state joining process that uses frictional heat generated between a rotating tool and the workpiece to create a welded joint. Unlike traditional fusion-welding processes that involve melting the base metal, FSW achieves bonding through intense plastic deformation of the material without reaching its melting point.
One of the significant advantages of FSW is its ability to join materials that are considered difficult or impossible to weld using conventional methods. It has been successfully used on aluminum alloys, copper alloys, magnesium alloys, stainless steels, and even titanium alloys. FSW produces highly robust joints with excellent mechanical properties while avoiding defects associated with fusion welding techniques such as porosity or solidification cracking.
Another advantage of FSW is its energy efficiency compared to other welding processes since it does not require additional heating sources like gas flames or electric arcs. This results in lower operating costs over time. Additionally, FSW offers reduced distortion due to its low heat input nature.
Despite these benefits, FSW also has limitations. It requires specialized equipment capable of applying sufficient axial force onto the rotating tool during welding. Furthermore, because it relies on mechanical stirring rather than melting metal together entirely like traditional fusion techniques do; it may not be suitable for all applications where complete fusion is required.
Laser beam welding (LBW):
Laser beam welding (LBW) is an advanced technique that utilizes a highly focused laser beam as a heat source to join materials together. The laser beam rapidly heats and melts the workpiece, creating a localized molten pool that solidifies into a weld joint upon cooling.
One of the significant advantages of LBW is its high precision and control over heat input. The narrow laser beam allows for precise targeting, resulting in minimal distortion and excellent joint quality. Additionally, LBW offers fast welding speeds due to the concentrated energy density of the laser beam.
LBW is particularly suitable for joining small or delicate components where heat-affected zones must be minimized. It has found applications in industries such as microelectronics, medical device manufacturing, and aerospace engineering. However, LBW may not be ideal for thicker materials or large-scale projects due to its limited penetration depth compared to other welding processes.
Plasma arc welding (PAW):
Plasma arc welding (PAW) is an advanced fusion-welding process that uses a highly concentrated ionized gas plasma arc as a heat source to create weld joints. Similar to gas tungsten arc welding (GTAW), PAW employs a non-consumable tungsten electrode and an external shielding gas.
One of the main advantages of PAW is its ability to produce high-quality welds with minimal distortion and good control over heat input. The plasma arc reaches higher temperatures than conventional GTAW arcs, allowing for deeper penetration and faster travel speeds when required.
PAW finds applications in various industries including aerospace, automotive manufacturing, and pipe fabrication due to its versatility on different materials such as stainless steel, carbon steel, aluminum alloys, titanium alloys, etc. However, setting up PAW equipment can be more complex than some other processes because it requires precise control over shielding gases and electrical parameters.
Submerged arc welding (SAW):
Submerged arc welding (SAW) is a widely used automatic or semi-automatic fusion-welding process that utilizes an electrically conductive flux layer covering the entire weld area. The arc is created between a continuously fed bare electrode wire and the workpiece, while the flux layer protects the molten metal from atmospheric contamination.
SAW offers excellent deposition rates and high-quality welds with minimal operator intervention. It is commonly used in heavy fabrication industries such as shipbuilding, structural steel construction, and pressure vessel manufacturing. SAW can join thick materials efficiently due to its deep penetration capability.
One of the main advantages of SAW is its ability to operate in mechanized or automated systems, increasing productivity and reducing labor costs. However, SAW requires proper ventilation due to the emission of smoke and fumes during welding. Moreover, it may not be suitable for thin materials or applications that require precise control over heat input.
Gas tungsten arc welding (GTAW):
Gas tungsten arc welding (GTAW), also known as Tungsten Inert Gas (TIG) welding, is a versatile fusion-welding process that uses a non-consumable tungsten electrode to create weld joints. GTAW relies on an external shielding gas to protect the molten metal from atmospheric contamination.
One significant advantage of GTAW is its exceptional control over heat input compared to other processes. This makes it suitable for joining thin materials without distorting or overheating them. GTAW produces high-quality welds with good aesthetic appearance due to its precise control over filler metal deposition.
Another advantage of GTAW is its versatility on various metals including carbon steel, stainless steel, aluminum alloys, nickel alloys, copper alloys, etc., making it widely applicable across different industries such as aerospace engineering and automotive manufacturing.
However, GTAW has some limitations as well. It typically requires more skill and experience than other processes due to its manual nature and greater sensitivity towards variations in torch positioning or travel speed. Additionally , GTAW can be slower than some other processes when high deposition rates are required.
Electroslag welding (ESW):
Electroslag welding (ESW) is a highly efficient fusion-welding process that utilizes the heat generated from an electric arc passing through a molten slag pool to join metals together. ESW is typically used for joining thick sections of materials, particularly in the construction of heavy steel structures such as bridges and offshore platforms.
One of the main advantages of ESW is its ability to produce deep full-penetration welds in a single pass without requiring edge preparation or multiple passes. This results in significant time and cost savings compared to other processes. Additionally, ESW offers excellent control over heat input due to the localized nature of the welding process.
However, ESW has some limitations. It requires specialized equipment and setup, including a water-cooled copper shoe that contains the molten slag pool during welding. Additionally, ESW may not be suitable for thin materials or small-scale applications due to its high heat input and limited flexibility.
Magnetic pulse welding (MPW):
Magnetic pulse welding (MPW) is a solid-state joining process that uses magnetic forces generated by high-energy pulses to create weld joints between two workpieces. MPW has gained attention for its ability to join dissimilar metals with minimal thermal distortion or metallurgical changes.
The principle behind MPW involves placing one workpiece on top of another with a small gap between them while applying an intense magnetic field through an electromagnetic coil surrounding both pieces. When an electrical current passes through the coil, it generates a rapid discharge that creates powerful repulsive forces between the two workpieces, causing them to collide at high speeds.
One key advantage of MPW is its capability to create strong bonds between different materials without melting them completely like traditional fusion-welding processes do. This makes it valuable for applications where heat-sensitive components need to be joined or when preserving material properties becomes critical.
Resistance spot welding (RSW):
Resistance spot welding (RSW) is a widely used process for joining metal sheets or plates by applying pressure and an electric current through copper alloy electrodes. The heat generated by the resistance to current flow causes the surfaces of the workpieces to melt, creating a weld joint upon cooling.
RSW offers several advantages in terms of simplicity, speed, and cost-effectiveness. It is commonly used in automotive manufacturing for body and chassis assembly due to its high-speed operation and ability to join dissimilar materials such as steel and aluminum.
However, RSW has limitations as well. It requires direct access to both sides of the joint being welded, limiting its applications on complex geometries or hard-to-reach areas. Additionally, RSW produces nuggets that are relatively small compared to other welding processes; therefore, it may not be suitable for thick materials or heavy-duty structural applications.
Stud welding:
Stud welding is a specialized process that allows fastening metal studs or pins onto another base metal without using additional fasteners like nuts or bolts. The stud is typically made from stainless steel or mild steel and has a threaded end for easy attachment of other components.
The stud welding process involves placing the stud against the base material and then rapidly heating both parts with an arc generated between them. When the stud reaches melting temperature along with a portion of the base material surface, they are pressed together under pressure until solidification occurs.
One significant advantage of stud welding is its ability to create strong connections quickly without damaging the opposite side of the workpiece since most operations take place only on one side. This makes it valuable in construction industries where accessibility might be limited or when aesthetics need to be maintained on visible surfaces.
Ultrasonic welding:
Ultrasonic welding uses high-frequency sound waves (ultrasonic vibrations) above 20 kHz to create localized heat at plastic joints, thereby bonding them together without using additional adhesives or fasteners. Ultrasonic energy is applied through a vibrating tool or horn that is pressed against the joint, causing rapid frictional heating and subsequent welding.
Ultrasonic welding offers several advantages in terms of speed, cleanliness, and ease of automation. It is commonly used in industries such as automotive manufacturing, electronics assembly, medical device fabrication, and packaging production.
Oxy-fuel gas cutting and welding:
Oxy-fuel gas cutting and welding processes involve the use of a fuel gas (such as acetylene or propane) combined with oxygen to produce an intense flame for cutting or joining metals. Oxy-fuel gas cutting uses a high-temperature flame to melt through metal plates along a predetermined path. Oxy-fuel gas welding utilizes the same principle but focuses on creating molten metal puddles between two workpieces to form a weld joint upon cooling.
One advantage of oxy-fuel gas cutting is its ability to cut thick materials quickly without requiring complex equipment or specialized skills. Additionally, oxy-fuel gas welding is versatile since it can be used on various metals including carbon steel, stainless steel, copper alloys, etc., making it widely applicable across different industries such as shipbuilding or construction.
However, both processes have limitations too. Oxy-fuel gas cutting produces significant amounts of heat-affected zones due to the broad nature of the flame; therefore may not be ideal for applications where minimal distortion or heat input are required. Additionally , oxy-fuel gas welding has lower deposition rates compared to other fusion-welding processes like arc welding techniques.
Welding metallurgy:
Welding metallurgy refers to the study of how materials behave during the welding process and how their properties change after being joined together. Understanding welding metallurgy is crucial for selecting appropriate filler materials, controlling heat input during welding operations , assessing potential defects or failures in welded joints , etc .
During the fusion-welding process , localized heating causes changes in material microstructure which directly impact mechanical properties such as strength, toughness , and corrosion resistance. These changes can be either advantageous or detrimental depending on the specific welding process, base material composition , heat input levels , etc .
By studying welding metallurgy , engineers and welders can optimize welding procedures to achieve desired mechanical properties in welded joints while avoiding problems like cracking, porosity, or brittleness . Techniques such as post-weld heat treatment (PWHT) or selecting appropriate filler materials based on their alloying elements play a significant role in controlling microstructural changes during welding.
Welding inspection and testing techniques:
Welding inspection and testing are essential steps to ensure the quality and integrity of weld joints. Various non-destructive testing (NDT) methods are used to detect potential defects or discontinuities that might compromise the performance of welded structures.
Common NDT techniques include visual inspection, liquid penetrant testing (LPT), magnetic particle inspection (MPI), ultrasonic testing (UT), radiography, eddy current testing (ECT), etc. Each method has its advantages and limitations depending on factors such as accessibility, sensitivity required, type of defect being inspected for ,etc .
Visual inspection is the most basic form of examination but plays a crucial role in identifying obvious surface defects like cracks or lack of fusion. LPT uses capillary action to draw a colored dye into surface-breaking defects for easy detection under UV light . MPI relies on applying ferromagnetic particles onto surfaces with magnetic fields to reveal any surface-breaking defects.
Ultrasonic testing utilizes high-frequency sound waves that travel through materials detecting internal flaws such as voids or lack of fusion by analyzing reflected signals. Radiography involves exposing weldments to X-rays or gamma rays which penetrate through materials revealing internal discontinuities for interpretation . ECT detects surface-breaking cracks by inducing electrical currents into conductive materials observing changes in electromagnetic fields near defect sites .
Welding automation and robotics:
Welding automation refers to the use of mechanized or robotic systems to perform welding operations instead of manual labor. Automation offers several advantages such as increased productivity, improved weld quality and consistency, reduced labor costs, and enhanced safety.
Robotic welding systems can be programmed to perform repetitive tasks with high precision and efficiency. They are commonly used in industries where large volumes of similar products need to be manufactured consistently, such as automotive assembly lines or heavy fabrication industries.
Automation technologies also include semi-automatic systems like welding positioners or manipulators that aid operators by providing better access to workpieces and reducing fatigue during welding.
Welding safety procedures and equipment:
Welding poses several hazards that require strict adherence to safety procedures and the use of appropriate personal protective equipment (PPE). The most common hazards associated with welding include exposure to ultraviolet (UV) radiation, infrared radiation , fumes, gases , sparks , molten metal splatter , electric shock , etc .
To minimize these risks, welders must wear suitable PPE like a welding helmet with a darkened lens for eye protection against UV radiation. Other essential PPE includes flame-resistant clothing (such as leather jackets or aprons), gloves made from heat-resistant materials , respirators or masks for respiratory protection against fumes and gases generated during welding processes .
Additionally , proper ventilation should be maintained in the workspace through local exhaust ventilation systems or general dilution ventilation . Welding areas should be separated from non-essential personnel by establishing designated work zones protected by barriers . Regular inspections of equipment grounding cables should also be performed along with maintaining safe distances from flammable materials.
Employers are responsible for ensuring that workers receive adequate training on safe working practices while providing them with well-maintained equipment and facilities. Supervisors must enforce proper safety protocols throughout all stages of the welding process.
Welding defects and troubleshooting:
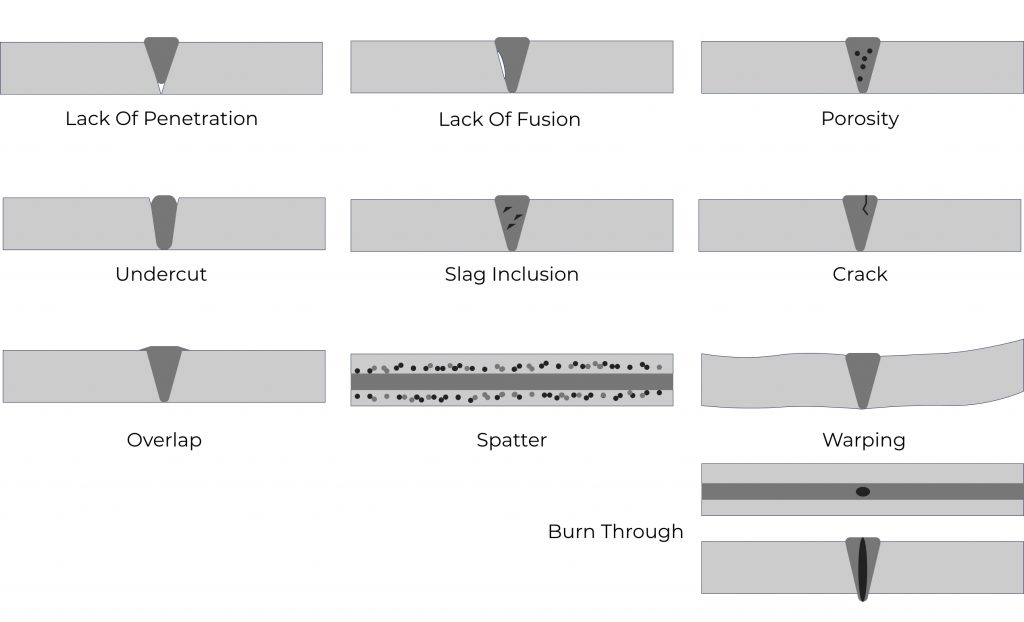
Welding defects refer to imperfections in welded joints that compromise their mechanical properties or structural integrity. Common defects include lack of fusion, porosity, cracks, undercutting, excessive spatter , etc .
Lack of fusion occurs when the weld metal does not properly bond with the base material or adjacent weld passes. This defect weakens the joint and can lead to cracking or failure under load.
Porosity refers to trapped gas bubbles within the weld metal that compromise its strength and corrosion resistance. Porosity can be caused by inadequate shielding gas coverage, improper cleaning of base materials , contaminated filler metals or fluxes , etc .
Cracks are often a serious concern as they significantly reduce the strength and integrity of welded joints . They can occur during welding due to high residual stresses , rapid cooling rates , or hydrogen embrittlement from moisture contamination in electrodes /fluxes .
Undercutting happens when excessive melting at the edges of a joint causes a groove-like depression along its length. Undercutting undermines the mechanical strength and fatigue resistance of welded structures.
Excessive spatter is an annoyance as it creates unnecessary cleanup work but doesn’t necessarily affect structural integrity . It is caused by improper shielding gas flow rates , electrode stick-out length being too long , contaminated surfaces/ consumables .
To troubleshoot welding defects, analyzing their root cause is crucial. Often, adjustments need to be made to welding parameters such as current settings, travel speed , preheat temperatures , interpass temperatures, etc., depending on specific defect types . Additionally proper fit-up (joint preparation) should be ensured for good penetration into base materials avoiding gaps or misalignment issues.
Non-destructive testing in welds:
Non-destructive testing (NDT) techniques play a vital role in evaluating the quality and integrity of weld joints without causing any