“Mastering the Art of Quenching: 8 Tips for Effective Tool Steel Manufacturing”
Quenching is a crucial process in tool steel manufacturing that helps achieve the desired hardness and performance characteristics. Understanding the principles and techniques of quenching is essential for modern blacksmiths to produce high-quality tools. In this article, we will explore the top 8 tips for effectively quenching tool steels.
1. Choose the right type of tool steel:
Not all tool steels are created equal when it comes to quenching. Different grades have varying compositions and properties, which influence their response to heat treatment. Before starting the quenching process, it’s important to select a suitable grade of tool steel that aligns with your specific requirements.
The most commonly used types of tool steels for blacksmithing include O1, A2, D2, and S7. Each has its own unique characteristics and should be handled differently during quenching.
2. Preheat before hardening:
Preheating the workpiece before hardening can help minimize thermal shock during quenching and reduce the risk of cracking or warping. This step ensures a more uniform temperature distribution throughout the steel.
To preheat your tool steel, place it in a furnace or heat treat oven at a temperature between 800-1100°F (427-593°C) for an appropriate amount of time depending on its size and thickness.
3. Use proper heating techniques:
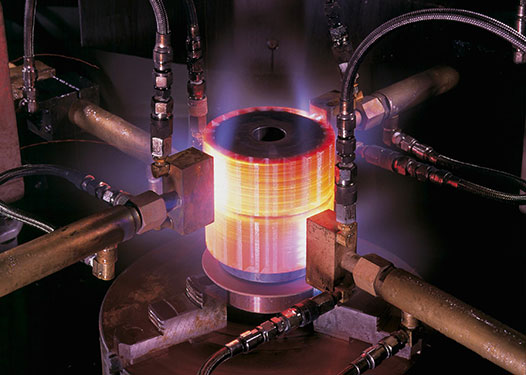
Achieving optimal hardness depends on heating your tool steel correctly. The most common method is through direct contact with flames or using an induction coil or electric furnace.
When using an open flame, ensure even heating by moving the workpiece back and forth across the flame rather than keeping it stationary in one spot. This helps prevent localized overheating which can lead to uneven hardness after quenching.
For larger pieces or complex shapes where precise temperature control is necessary, induction heating or electric furnaces provide more consistent results due to their ability to maintain stable temperatures.
4. Monitor austenitizing temperature:
Austenitizing temperature is the critical point at which the tool steel transforms into its austenite phase, allowing for proper hardening. It varies depending on the specific type of tool steel being used.
It’s crucial to closely monitor and maintain the austenitizing temperature within a narrow range recommended by the manufacturer. Deviating from this range can result in incomplete transformation or grain growth, both of which negatively impact hardness and toughness.
5. Quenching methods:
There are several quenching methods commonly employed when working with tool steels:
a) Oil quenching: This method uses oil as a cooling medium due to its ability to extract heat more slowly, reducing the risk of cracking or distortion. Different types of oils such as mineral oil, vegetable oil, or specialized quenching oils are available based on desired hardness requirements.
b) Water quenching: Water is an effective cooling medium that provides rapid heat extraction but can create higher thermal stresses compared to oil quenching. Care should be taken when using water as it may cause severe distortion or cracking if not properly executed.
c) Polymer quenchants: Polymer solutions like water-based polymer emulsions offer controlled cooling rates similar to oil while providing enhanced safety benefits over traditional oils due to their lower fire hazard properties.
The choice of quenching method depends on factors such as desired hardness level, steel grade, part geometry, and personal preference. Experimentation and experience will help you determine what works best for your specific applications.
6. Avoid sudden movements during quenching:
During the immersion stage of quenching, it’s important to avoid any sudden movements that could lead to uneven cooling rates and potential distortion or cracking. Slowly immerse your workpiece into the chosen quenchant in a smooth motion until fully submerged.
7. Agitation techniques:
Agitating the workpiece during quenching can improve heat transfer and reduce the formation of vapor barriers, known as steam jackets. These steam jackets can inhibit proper cooling and negatively affect hardness.
Methods such as gentle stirring or vertical oscillations in the quenchant can help break up these steam jackets, allowing for more effective cooling. However, be cautious not to create excessive turbulence that might cause distortion or splashing of the quenchant.
8. Post-quenching processes:
After completing the quenching process, it’s essential to perform additional steps to achieve desired properties:
a) Tempering: Tool steels are typically too hard and brittle after quenching. Tempering involves reheating the steel to a specific temperature range below its critical point and holding it there for a designated period. This relieves internal stresses, increases toughness, and reduces brittleness while maintaining an acceptable level of hardness.
b) Cryogenic treatment: Optional but highly beneficial, cryogenic treatment involves subjecting the tool steel to extremely cold temperatures (around -300°F or -184°C) for an extended period. This further refines microstructures and enhances wear resistance by converting retained austenite into martensite.
c) Surface finishing: Finally, consider surface finishing techniques like grinding or polishing to remove any scale or decarburization formed during heating and quenching processes. A smooth surface not only improves aesthetics but also reduces friction during use.
In conclusion, mastering the art of quenching tool steels is crucial for achieving optimum hardness levels required in various blacksmithing applications. By selecting suitable grades of steel, employing appropriate heating techniques, closely monitoring temperatures throughout each stage of heat treatment, choosing appropriate quenchants and agitating methods when necessary—blacksmiths can ensure their tools possess superior strength, durability, and performance characteristics demanded by professionals across industries where they’re employed