Exploring the Advantages and Disadvantages of Oxy-Fuel Cutting in Metalworking Industry
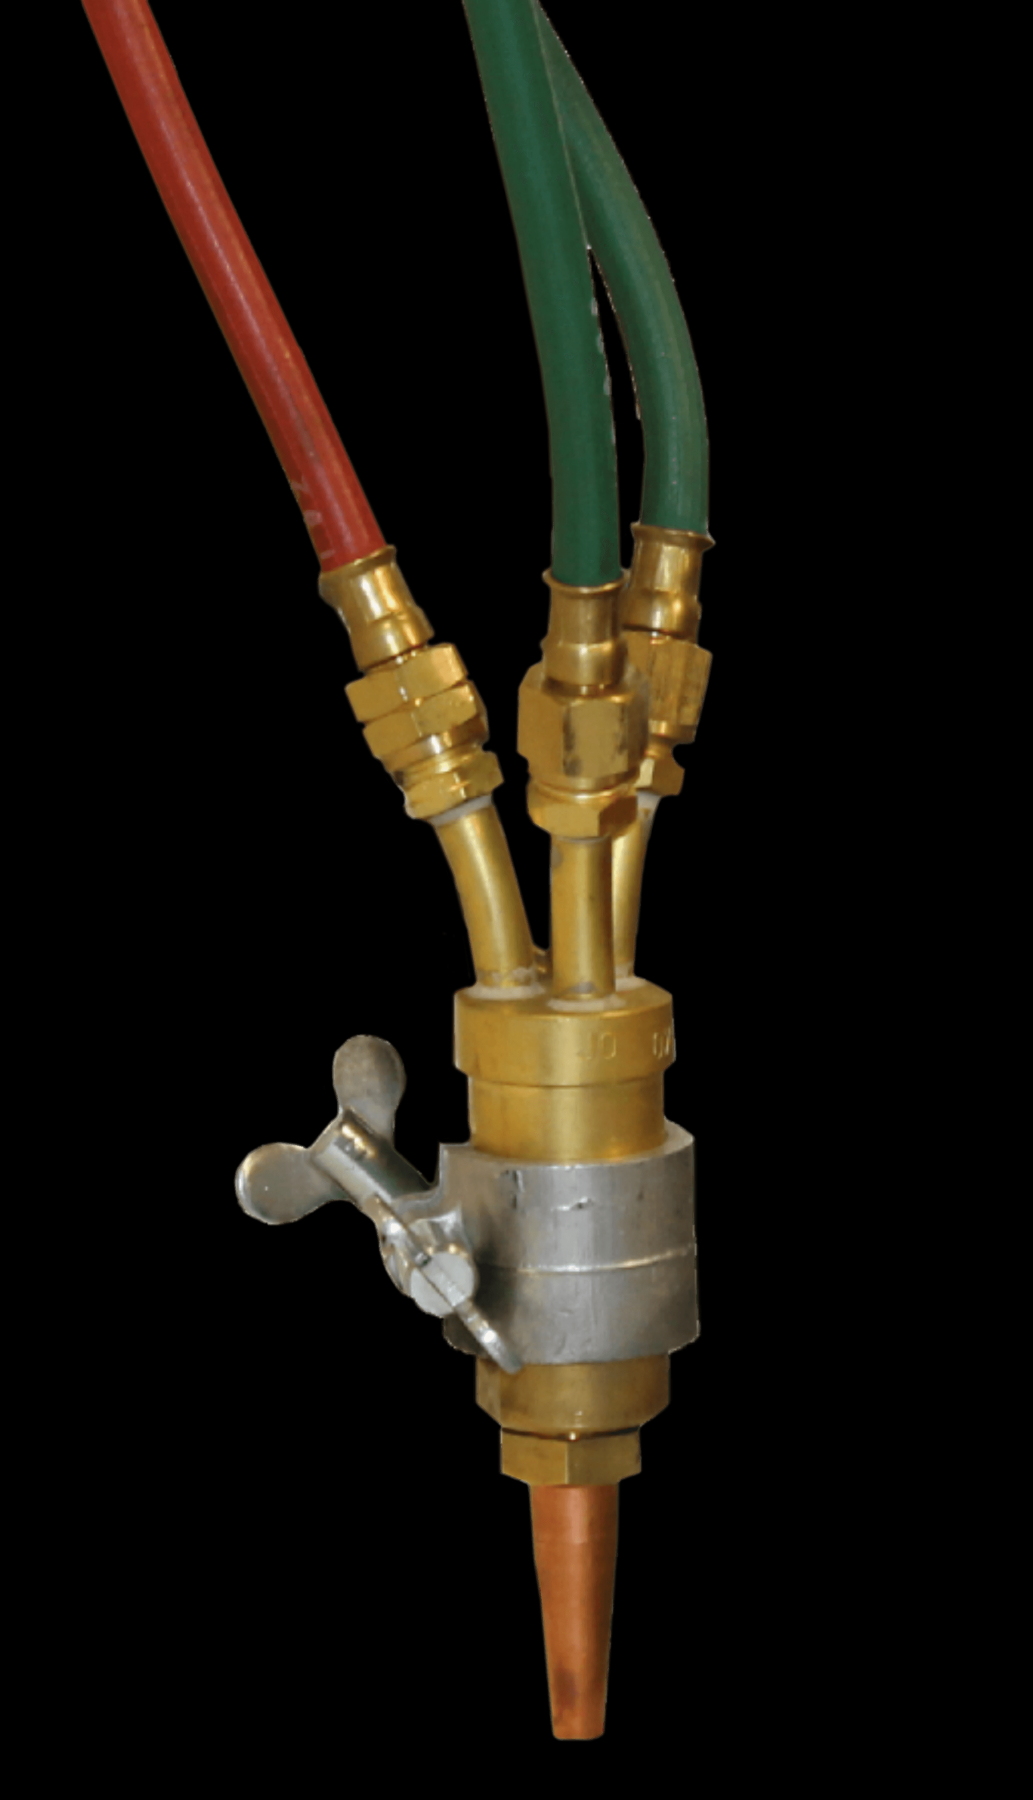
Oxy-fuel cutting is a popular technique that has been used for many years in the metalworking industry. It involves the use of oxygen and fuel gases, such as acetylene or propane, to create a flame that can be used to cut through various metals.
In this article, we will explore what oxy-fuel cutting is, how it works, its advantages and disadvantages, and some tips on how to use it effectively.
What Is Oxy-Fuel Cutting?
Oxy-fuel cutting is a thermal cutting process that uses heat from a flame produced by mixing pure oxygen with one of several fuel gases. The most common fuel gas used in oxy-fuel cutting is acetylene because it produces the highest temperature flame.
The process involves heating the metal to its ignition point using an intense flame created by combining oxygen with fuel gas. Once heated sufficiently, the metal melts and then oxidizes or burns away due to the presence of pure oxygen in the flame.
How Does Oxy-Fuel Cutting Work?
Oxy-fuel cutting requires three main components: an oxygen source, a combustible gas source (typically acetylene), and a torch head capable of mixing both gases together before igniting them into a high-temperature flame.
As mentioned earlier, acetylene is commonly used as the combustible gas source due to its ability to produce high temperatures when mixed with pure oxygen. The two gases are fed into separate hoses connected at their respective regulators before being combined into one hose leading up to the torch head.
Once ignited using either flint striker or electronic sparkler based on type of equipment being utilized; Heating from this single stream tip creates an exothermic reaction between iron oxide coating applied on surface which causes oxidation while burning off excess material until desired depth reached thus allowing precise cuts without overheating workpiece directly underneath nozzle area but also producing slag formation due lack control over combustion speed causing deformation unevenness along edges.
Advantages of Oxy-Fuel Cutting
There are several advantages to using oxy-fuel cutting over other types of cutting methods such as plasma, laser, or water jet cutting. Here are some benefits that make oxy-fuel cutting a popular technique among metalworkers:
1. Cost-effective: Oxy-fuel cutting is one of the most cost-effective ways to cut through thick metals compared to other techniques like laser and water jet cutting.
2. Easy to use: Oxy-fuel equipment is relatively easy to set up and operate, making it a great option for beginners who want to learn how to cut metal.
3. Portable: The equipment used in oxy-fuel cutting can be easily transported from one location to another, making it ideal for on-site work.
4. Versatile: Oxy-fuel torches can be used with various fuel gases, allowing you to adjust the flame’s temperature according to your needs.
Disadvantages of Oxy-Fuel Cutting
While there are several advantages associated with oxy-fuel cutting, there are also some disadvantages you should consider before choosing this method:
1. Limited precision: Unlike other types of thermal and non-thermal techniques such as laser and water jet cutting methods which offer higher precision cuts without slag formation on edges; due lack control over combustion speed causing deformation unevenness along edges resulting in limited accuracy during cuts when working with complex patterns or designs requiring high degree accuracy.
2. Slow-speed process: Compared with other thermal techniques like plasma or laser cutter, oxyfuel method takes longer time since burning off excess material until desired depth reached thus causing slow speed process overall productivity may decrease significantly if project involves large volume production runs.
3. Safety concerns: As we’re dealing with flammable gases involved in the process so safety precautions must always be taken when handling oxygen tanks connected hoses leading up nozzle area where intense heat produced by igniting mixture required proper ventilation space between tank gas source and work area thus preventing any kind of possible accident.
Tips for Using Oxy-Fuel Cutting Effectively
To use oxy-fuel cutting effectively, here are some tips to consider:
1. Select the right tip size: Choosing the right tip size is crucial in determining the quality of your cuts. A too small tip can cause overheating, while a too large one can reduce accuracy. Always select the appropriate nozzle according to thickness being cut and desired precision level required by project needs.
2. Maintain correct gas pressure: Maintaining proper gas pressure is important for optimal performance during cutting operations; it helps ensure that the flame stays consistent throughout the process.
3. Keep the torch perpendicular to the metal surface: Keeping your torch perpendicular to your workpiece will help you achieve straighter cuts along with avoiding slag formation on edges due unevenness caused by distorted angles.
4. Use protective equipment: As mentioned earlier safety precautions must always be taken when handling oxygen tanks connected hoses leading up nozzle area where intense heat produced by igniting mixture required proper ventilation space between tank gas source and work area thus preventing any kind of possible accident so wearing personal protective equipment such as goggles, gloves, and flame-resistant clothing is crucial while working with oxy-fuel cutting method.
Conclusion
Oxy-fuel cutting is an effective technique used widely in metalworking industry due its cost-effectiveness, ease-of-use and portability making it ideal choice for beginners or small-scale projects requiring high degree accuracy but not suitable for complex patterns or designs since limited precision compared with other thermal techniques like plasma or laser cutter methods which offer higher precision cuts without slag formation on edges resulting in reduced productivity volumes if project involves large production runs where speed becomes key factor affecting overall efficiency during manufacturing processes .